China Top OEM Sheet Metal Deep Drawing Factory & Exporter

ISO 9001:2015 Certified Precision Stamping, Hydroforming & Deep Drawn Components Engineering Whitepaper | 16+ Years Sourcing Excellence

Precision Deep Drawn & Stamped OEM Product Suite

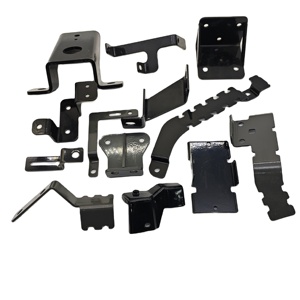
Explore our flagship OEM sheet metal fabrication capabilities. Operating under high-tonnage hydraulic presses and ultra-precise progressive dies, our factory processes stainless steel, aluminum alloys, copper, and carbon steel into highly complex cylindrical, box, and contoured geometries.
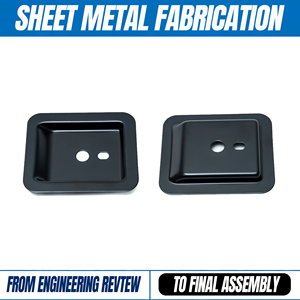
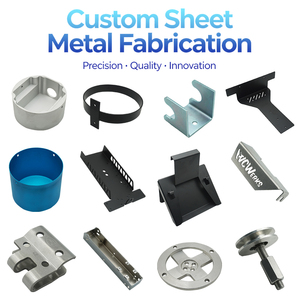
ISO 9001 Certified Factory Custom Sheet Metal Fabrication Stamping & Deep Drawing Services
ISO 9001 Certified
Custom Sheet Metal Fabrication Stamping & Deep Drawing Services
Deep drawn enclosures, automotive components, and structural housings engineered to ±0.01mm tolerances.
Inquire Now
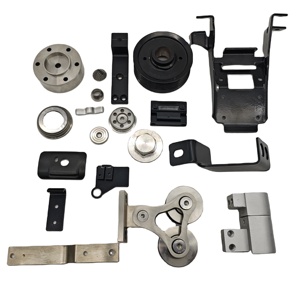
Warrior Hardware OEM EDM Custom Precision Steel Aluminum Stamping Deep Drawing Parts
Wire EDM Precision
EDM Precision Steel & Aluminum Deep Drawing Hardware Parts
High-volume precision hardware with custom tooling, deburring, and anti-corrosion surface treatments.
Inquire Now
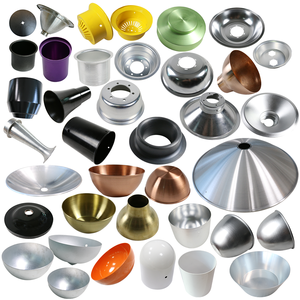
Custom OEM Sheet Metal Stamping Aluminium Stainless Steel Copper Deep Drawing Drawn Parts
Multi-Material OEM
Aluminum, Stainless Steel & Copper Deep Drawn Structural Parts
Seamless cold drawing of non-ferrous metals and stainless grades for HVAC, electrical, and culinary gear.
Inquire Now
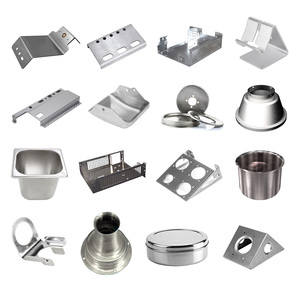
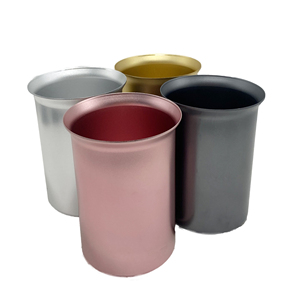
Custom Sheet Metal Fabrication Processing Aluminum Alloy Sheet Metal Stamping Deep Drawing Parts
Alloy Processing
Aluminum Alloy Stamping & Deep Drawing Processing Components
High-strength aluminum 5052/6061 drawing with post-forming anodizing and thermal treatment.
Inquire Now
YW Hardware OEM Sheet Metal Stamping Deep Drawing Parts 304 316 Stainless Steel Carbon Steel Custom Fabrication
304 / 316 Stainless
304 / 316 Stainless & Carbon Steel Custom Deep Drawing Hardware
Heavy-duty drawn canisters, pressure-tested vessels, and industrial bracketry built for harsh environments.
Inquire Now
Deep Draw Steel Q235 Sheet Metal Fabrication CNC Spinning Hydroforming Brushed Surface
CNC Spinning & Hydroforming
Deep Draw Q235 Steel CNC Spinning & Hydroforming Large Shells
1.4mm+ thick structural steel forming combining hydroforming, CNC spinning, and fine brushed finishing.
Inquire Now
16 Years Stamping Factory Direct Custom Sheet Metal Deep Drawing Parts
16+ Years Factory Direct
Factory Direct Custom Stainless Steel & Aluminum Deep Drawn Parts
Direct OEM manufacturing eliminating intermediary margins, supported by complete in-house die toolmaking.
Inquire Now
OEM Custom Deep Drawing Laser Cutting Service Sheet Metal Fabrication Metal Stamping Parts
Laser Cut & Deep Draw
Integrated Laser Cutting, Stamping & Deep Drawing OEM Assembly
Hybrid manufacturing combining fiber laser blanking, multi-stage deep drawing, and automated welding.
Inquire Now

Factory Infrastructure & Technical Benchmarks

As a leading Chinese OEM sheet metal deep drawing manufacturer and global exporter, our facility operates at the nexus of metallurgical science and advanced mechanical engineering. Vertically integrated from raw material blanking to final surface passivation, we produce over 500,000 kg of processed metal components monthly for Fortune 500 enterprises and specialized B2B brands across North America, Europe, and Asia-Pacific.

16+
Years Experience
500K
Monthly Kg Output
±0.01
Precision Limit (mm)
100%
Lab Tested Quality
15+
Export Markets
In-House Tooling & EDM
Equipped with slow-feed Wire EDM, CNC machining centers, and dedicated master die-makers to turn complex CAD models into production-ready progressive tooling within 15–21 days.
Rigorous Metrology Lab
CMM (Coordinate Measuring Machines), optical spectrum analyzers, salt spray testers, and tensile strength testers guarantee 100% compliance with ASTM, DIN, and ISO standards.
Multi-Process Capability
From hydraulic deep drawing (up to 800-ton capacity) and CNC metal spinning to hydroforming, laser trimming, and robotic TIG/laser welding—all executed under one roof.

Technical Deep Dive: Mechanics of Deep Drawing & Material Dynamics

Deep drawing is a radial-draw metal forming process where a flat sheet metal blank is mechanically pulled into a forming die by a punch. Achieving structural integrity without flange wrinkling, wall thinning, or tensile necking requires precise control over the Limiting Draw Ratio (LDR), blank holder pressure (BHP), lubrication friction coefficients, and anisotropy (r-value) of the alloy.

1. Limiting Draw Ratio (LDR) & Multi-Stage Reductions

The maximum ratio of blank diameter ($D_b$) to punch diameter ($d_p$) dictates whether a part can be formed in a single stroke or requires multi-stage progressive drawing with intermediate anneals. For standard AISI 304 austenitic stainless steel, the maximum single-draw reduction is typically $LDR \approx 2.0 - 2.2$ (approx. 45%–50% diameter reduction). When deep shell aspect ratios exceed 1:1 ($Depth:Diameter$), our engineering team calculates multi-pass reduction sequences using the following industrial guidelines:

Drawing Stage Max Diameter Reduction (%) Punch / Die Radius Ratio Recommended Lubrication Intermediate Annealing Requirement
1st Draw (Cupping) 40% – 48% 4t to 8t (t = sheet thickness) High-viscosity chlorinated oil / Polymer film Not required
2nd Draw (Redraw) 20% – 30% 3t to 6t Synthetic extreme-pressure lubricant Optional based on strain hardening
3rd Draw (Final sizing) 12% – 18% 2t to 4t Emulsified water-soluble oil Bright annealing required for 300-series SS
Ironing (Wall Sizing) 10% – 15% wall thickness reduction Sharp radius transition Micro-pigmented synthetic oil Stress-relief annealing post-ironing

2. Material Selection & Plastic Strain Anisotropy Matrix

Selecting the correct alloy state determines dimensional stability and surface topography post-draw. Below is a engineering comparative selection matrix used by our metallurgists during design-for-manufacturability (DFM) reviews:

Material Grade Yield Strength (MPa) Tensile Strength (MPa) Planar Anisotropy ($\bar{r}$) Formability & Application Ideality
AISI 304 / 304L Stainless 205 – 240 515 – 620 1.0 – 1.2 Exceptional work-hardening capacity. Ideal for food-grade vessels, medical shells, and chemical tanks.
AISI 316 / 316L Stainless 240 – 290 580 – 680 1.0 – 1.15 Superior molybdenum-enhanced chloride corrosion resistance. Preferred for marine hardware and pharmaceutical housings.
Aluminum 5052-O 90 – 110 190 – 230 0.6 – 0.85 Fully annealed state offering high ductility. Ideal for lightweight automotive oil pans and electronics shields.
SPCC / Q235 Carbon Steel 185 – 260 270 – 410 1.4 – 1.8 High normal anisotropy minimizing thinning. Excellent for deep automotive stamping, motor housings, and structural brackets.
C26000 Cartridge Brass 110 – 150 300 – 380 0.9 – 1.0 Superb deep drawability with low tool wear. Used in electrical connectors, plumbing fittings, and decorative caps.
Engineering Tip: Preventing Earing & Wrinkling

Planar anisotropy ($\Delta r$) causes non-uniform edge height (earing) during deep cylindrical drawing. Our engineering team utilizes finite element analysis (FEA) via AutoForm software to optimize blank layouts and variable binder pressure profiles, eliminating material waste by up to 14% and suppressing flange wrinkling without over-stressing wall boundaries.

Global Sourcing Trends & Next-Gen Manufacturing Evolution

Global industrial supply chains are transitioning from transactional purchasing to strategic co-engineering partnerships. For procurement executives and engineering directors sourcing OEM deep drawing components from China, four macro-trends are defining competitiveness through 2030:

1. Smart Servo Presses & Dynamic Cushion Control
Traditional mechanical flywheel presses are being replaced by high-tonnage CNC servo presses. Servo-driven motion profiles allow variable velocity during the punch-to-blank impact phase, drastically reducing material shock strain, eliminating micro-cracking in high-strength alloys, and improving wall thickness uniformity by up to 22%.
2. Hybrid Hydroforming-Spinning Integration
For non-symmetric or ultra-deep components, combining hydraulic fluid pressure forming (hydroforming) with secondary CNC metal spinning reduces tooling costs by 40% compared to massive multi-stage progressive stamping dies, enabling cost-effective medium-to-high volume production runs.
3. Green Aluminum & Recyclability Audits
International ESG mandates (such as Europe’s CBAM framework) demand full carbon transparency. Modern OEM factories are adopting closed-loop scrap recycling systems, clean lubrication systems (dry-lube films), and certified low-carbon raw material billets to lower Scope 3 embedded carbon emissions.
4. Real-time In-Die Metrology & AI Defect Detection
Integrating piezoelectric force sensors and optical laser scanners directly inside stamping dies enables real-time detection of blank slippage, burr height degradation, or material thickness variations. Non-conforming parts are automatically ejected, achieving near-zero PPM defect rates for global OEMs.

Procurement Framework: Total Cost of Ownership (TCO) Analysis

Evaluating an overseas OEM deep drawing supplier solely on unit piece price creates hidden cost risks. Procurement teams must evaluate the complete TCO lifecycle, factoring in tooling amortization, yield scrap rates, surface finishing failures, and transit protection costs.

Cost Component Low-Cost Tier 3 Supplier Warrior / Enterprise OEM Factory Strategic Risk & Value Impact
Tooling Investment & Life Low initial price (Soft steel tooling, 50k-100k cycles) Optimized tooling (Cr12MoV / SKD11 tool steel, 500k-1M+ cycles) Inferior tooling leads to dimensional drift, burrs, and premature die replacement costs.
Material Traceability Uncertified secondary market coils 100% Prime Mill Certificates (Baosteel, TISCO, POSCO) Inconsistent yield strengths cause erratic springback and high scrap rates on assembly lines.
Secondary Processing Subcontracted plating/polishing (Uncontrolled Ra) In-house automated polishing, passivation, anodizing Ensures stable surface roughness (Ra < 0.4 µm) and zero intergranular corrosion issues.
Export Packaging Basic corrugated cartons without rust prevention VCI (Vapor Corrosion Inhibitor) bags + custom foam + ocean crates Prevents oxidation, scratching, and salt vapor pitting during 30-45 day ocean freight transit.

Frequently Asked Questions (OEM Deep Drawing Sourcing)

Clear, technical answers to common engineering and procurement inquiries regarding deep drawing sheet metal fabrication.

What is the maximum drawing depth and wall thickness your factory can achieve?
Our facility operates hydraulic presses ranging from 100 tons to 800 tons. We can deep draw shell depths up to 400mm and process metal thicknesses from 0.3mm to 6.0mm for soft steels, aluminum, and copper. For 300-series stainless steel, our typical max draw depth in a single pass depends on the shell diameter, maintaining drawn wall thickness tolerances within ±0.03mm across multi-stage operations.
How do you prevent wrinkling, tearing, and earing in stainless steel deep drawn parts?
We employ a three-tier mitigation strategy: First, we conduct AutoForm FEA simulation to optimize blank shape and calculate variable binder force profiles. Second, we utilize specialized die steels (SKD11/D2 or Carbide) with micro-polished draw radii (Ra < 0.2 µm). Third, we utilize high-pressure synthetic extreme-pressure (EP) lubricants and select materials with controlled grain structures ($r$-value $\ge 1.2$) to ensure uniform plastic strain without localized thinning.
What dimensional tolerances can your deep drawing process maintain?
For standard production runs, we maintain ISO 2768-m (Medium) to ISO 2768-f (Fine) tolerances. Critical internal and external diameters can be held to ±0.02mm using secondary CNC re-striking or ironing passes. Hole positions, flange flatness, and total height can be maintained to ±0.05mm depending on component geometry and material thickness.
What surface finishes and post-processing treatments do you provide in-house?
We provide end-to-end surface finishing including mechanical mirror polishing (up to #8 mirror finish), brushed/satin finishing, electropolishing, chemical passivation (ASTM A967), anodizing (Type II & Type III hardcoat for aluminum), powder coating, electroplating (zinc, nickel, chrome), and laser engraving.
What are your typical lead times for tooling prototyping and mass production shipments?
Rapid prototype samples produced via CNC spinning, soft tooling, or laser-welded blanking can be delivered within 7 to 10 working days. Full production progressive or compound deep drawing tooling requires 20 to 35 days, including T1 sample testing and inspection reporting. Once tooling is approved, mass production orders are fulfilled in 15 to 25 days depending on batch volume.
How do you guarantee material quality and raw alloy authenticity?
Every batch of raw material metal sheet or coil is acquired from Tier-1 certified steel mills (such as Baosteel, TISCO, or POSCO) accompanied by authentic Mill Test Certificates (MTC) conforming to EN 10204 3.1. Before blanking, our internal quality laboratory validates material composition using an optical emission spectrometer and conducts tensile strain testing.
What CAD/CAM file formats does your engineering department accept for DFM review?
We accept all standard 3D CAD formats, including STEP (.stp / .step), IGES (.igs), SolidWorks (.sldprt), Parasolid (.x_t), and 2D engineering drawings in DWG or DXF format (with GD&T callouts). Our engineering department returns a detailed DFM analysis report within 24 hours.
Can your factory handle complex hybrid assemblies involving deep drawing, laser cutting, and welding?
Yes. In addition to deep draw press lines, our 12,000 m² factory houses 6kW fiber laser cutters, 5-axis CNC machining centers, robotic TIG/MIG welding cells, and automated laser spot welding machines. We routinely manufacture complete sub-assemblies featuring drawn housings welded to mounting flanges and internal bracketry.

Transform Your Sheet Metal Designs Into Production-Grade OEM Components

Partner with China’s premier ISO 9001 certified deep drawing and metal stamping manufacturer. Send us your CAD drawings or technical specifications today for a comprehensive DFM evaluation and transparent factory-direct quotation within 24 hours.

Inquire Now