Engineering Precision Stainless Steel Products
Manufactured via multi-stage deep drawing, precision edge trimming, and automated electropolishing. Designed to meet stringent European standards (EN 10088 / ISO 9001).
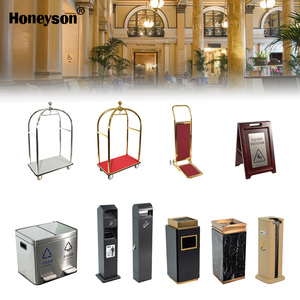
Star Hotel Supplies Full Set Stainless Steel Hotel Equipment
- Material: AISI 304 / AISI 201
- Process: Deep Drawing & Hybrid Assembly
- Surface: Satin Brush / Mirror Polish
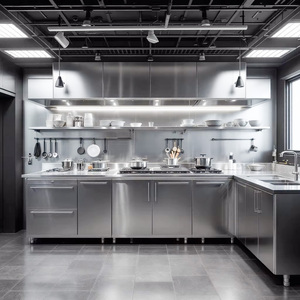
Customized Restaurant Kitchen Deep Drawn Steel Equipment
- Seamless Deep Drawn Basins
- High Thermal & Mechanical Resistance
- Custom Gauge: 0.8mm to 1.5mm
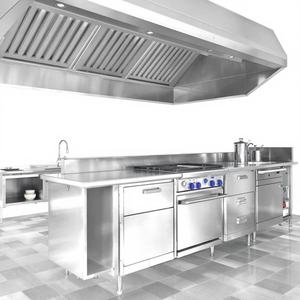
Commercial Hotel & Restaurant All-in-One Equipment Units
- Integrated Deep Drawn Worktops
- Corrosion Resistant Grade 304
- OEM / ODM Mold Customization
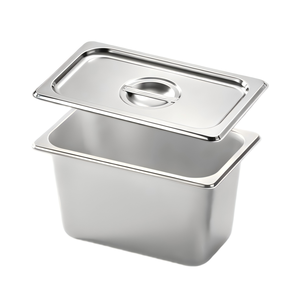
1/4 150mm Gastronorm GN Pan Deep Drawn Food Container
- Standard EN 631 EU Specification
- Uniform Wall Thickness Control
- Stackable Anti-Jamming Rim Design
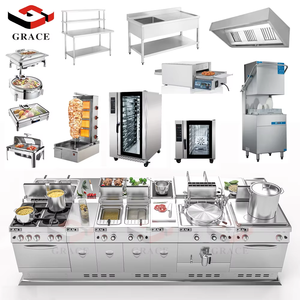
GRACE Heavy-Duty Industrial Kitchen Equipment Set
- Deep Drawn Stainless Steel Modules
- Ideal for Fast Food & Catering
- High Tensile Stamping Strength
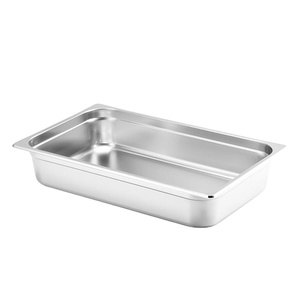
Standard 1/1 Gastronorm 304/201 Commercial GN Pan
- Deep Drawn Radii for Easy Cleaning
- Electropolished Internal Finish
- NSF / Food Grade Compliance
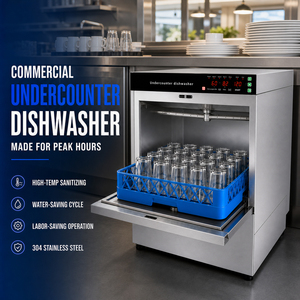
Under-Counter Commercial Dishwasher Deep Drawn Tank
- One-Piece Drawn Water Basin
- Leak-Proof Hydro-Formed Structure
- High-Volume Commercial Grade
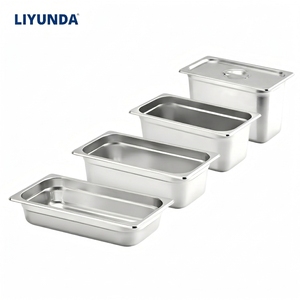
Precision EU GN Pan 1/3 Deep Drawn Container
- Ultra-Smooth Deep Drawn Cornering
- Precision Flange Dimensioning
- In-House Die Stamp Quality
Engineering Mechanics of Stainless Steel Deep Drawing in Modern Manufacturing
Deep drawing is a fundamental metal cold-forming process where flat stainless steel sheet metal blanks are radially drawn into a forming die by a mechanical or hydraulic punch. The transformation involves complex plastic deformation, requiring precise control over sheet metal strain hardening rates, blank holder forces (BHF), draw ratios, and interfacial lubrication friction. In high-volume B2B manufacturing—ranging from commercial Gastronorm containers to automotive pressings and pressure vessel domes—mastering these metallurgical variables is essential for preventing wrinkling, localized necking, or catastrophic ductile fracture.
Technical Principle: The Limit Draw Ratio (LDR) for austenitic stainless steel (such as AISI 304/316) typically ranges between 2.0 to 2.2 in initial draw stages. Achieving deep cavity depths without intermediate annealing requires precise die radius geometry ($R_d \approx 6t$ to $10t$) and automated hydraulic cushion regulation.
1. Material Selection & Metallurgical Characteristics
The choice of stainless steel alloy directly dictates drawability, corrosion resistance, and structural performance. Austenitic alloys (300 series) exhibit high work-hardening exponent values ($n \approx 0.45$ to $0.50$), making them exceptionally suited for deep stretching and deep drawing applications:
- AISI 304 / EN 1.4301 (Cr-Ni Alloy): The industry standard for food equipment, commercial cookware, and deep drawn sinks. High ductility, excellent drawability, and superior atmospheric corrosion resistance.
- AISI 316L / EN 1.4404 (Cr-Ni-Mo Low Carbon): Formulated with 2-3% Molybdenum for enhanced resistance against pitting corrosion in chloride-rich environments, ideal for marine components, pharmaceutical tanks, and chemical processing parts.
- AISI 201 / Low-Nickel High-Manganese: Cost-optimized alloy suitable for high-volume commercial catering pans, offering higher yield strength ($R_{p0.2} \ge 350\text{ MPa}$) with controlled deep draw characteristics.
2. Deep Drawing Tooling Parameters & Technical Specifications
Below is an empirical specification matrix representing our standardized deep drawing tooling tolerances, thickness limits, and hydraulic press parameters for custom OEM parts.
| Engineering Parameter | Standard Capability | Precision / High-Spec Capability | Quality Verification Method |
|---|---|---|---|
| Material Sheet Thickness ($t$) | 0.4 mm – 3.0 mm | 0.3 mm – 6.0 mm | Ultrasonic Gauge / Micrometer |
| Max Depth of Draw ($H$) | Up to 350 mm (Single/Double Action) | Up to 500 mm (Multi-Stage with Annealing) | Optical 3D Coordinate Scanner |
| Dimensional Tolerance | ISO 2768-m (±0.2 mm) | Precision ISO 2768-f (±0.05 mm) | Coordinate Measuring Machine (CMM) |
| Pressing Tonnage Range | 100 Tons – 500 Tons | 800 Tons Servo-Hydraulic | Load Cell Pressure Transducers |
| Die Radius ($R_d$) Clearance | $c = t + 0.07\sqrt{10t}$ | Custom CNC Ground Radius ($\pm 0.01\text{ mm}$) | Profilometer Surface Gauge |
| Surface Polish Finish | 2B Mill Finish / Satin Brush (Ra 0.4µm) | Electro-Polished / Mirror (Ra < 0.1µm) | Surface Roughness Tester |
3. Preventing Wall Thinning & Wrinkling
During deep drawing, sheet metal under the blank holder is subjected to radial tensile stress and tangential compressive stress. If tangential compressive stress exceeds critical buckling limits, peripheral wrinkling occurs. Conversely, excessive blank holder pressure causes severe friction over the punch nose radius, leading to localized necking and sidewall tearing.
Our engineering team utilizes finite element analysis (FEA) computer simulations to optimize blank geometry, calculate variable blank holding force profiles, and select high-grade synthetic water-soluble drawing lubricants containing extreme pressure (EP) additives.
In-House Bright Annealing
When draw ratios exceed 2.2, severe work hardening locks metal dislocation networks. Our continuous hydrogen atmosphere bright annealing furnace operates at 1050°C, restoring austenitic grain ductility without surface oxidation or scale formation.
Vertically Integrated Stainless Steel Manufacturing
From cold rolling raw stainless steel coils to high-speed deep draw stamping, custom tooling, and automated packaging.
500,000 kg Monthly Material Capacity
Supported by our parent group’s dedicated cold rolling mill facility, we process up to 500 metric tons of raw stainless steel sheets monthly. This upstream vertical integration ensures total material traceability, consistent gauge tolerances, and immunity against raw material market volatility.
In-House Tool & Die Making Shop
Equipped with high-precision 5-axis CNC machining centers, wire EDM, and surface grinders. Our team of veteran toolmakers crafts custom progressive dies, transfer dies, and deep draw punch assemblies to exacting client CAD drawings within tight lead times.
ISO & European Quality Certifications
Our quality management systems are fully certified according to ISO 9001:2015, CE food contact safety standards, RoHS, REACH, and BSCI social compliance guidelines. Every production batch undergoes 100% optical inspection and material spectral analysis.
Advanced OEM Customization & Private Label Packaging
We empower international B2B brands, commercial kitchenware importers, and industrial original equipment manufacturers to bring custom metal parts to market effortlessly. "You Design, We Manufacture"—from initial sample rapid prototyping to laser etching, surface passivation, and custom-branded export packaging.
- Custom laser logo engraving & part serialization
- Passivation & electropolishing for medical/food grade cleanliness
- Drop-test approved export carton & pallet packing
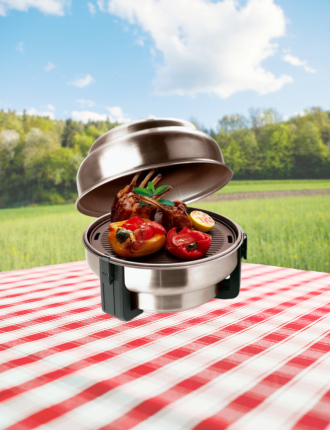
Deep Drawn Stainless Steel Components in Turkey's Industrial Sectors
Turkey has firmly established itself as a global manufacturing powerhouse and a strategic bridge between Europe, the Middle East, and Eurasia. Industrial clusters across Istanbul, Bursa, Izmir, Kocaeli, and Gaziantep represent some of the most dynamic engineering hubs for commercial appliances, automotive assembly, and HoReCa (Hotel, Restaurant, and Catering) equipment manufacturing.
Our precision deep-drawn stainless steel parts, Gastronorm food containers, commercial dishwasher tubs, and industrial stampings directly serve key Turkish localized applications:
1. Commercial HoReCa & Hospitality (Antalya & Istanbul)
Turkey’s thriving tourism sector in Mediterranean coastal regions like Antalya and Izmir demands premium, heavy-duty commercial kitchen setups. Our EN 631 standard deep-drawn Gastronorm pans, buffet food warmers, and stainless steel cookware are integral components for leading Turkish hotelware brands.
2. White Goods & Appliance OEM (Bursa & Manisa)
Turkey is one of Europe's largest manufacturers of domestic and commercial home appliances. We produce seamless deep-drawn dishwasher interior basins, washing machine drum shells, and coffee machine boilers with zero-leak hydro-formed geometry.
3. Automotive & Commercial Transport (Kocaeli & Marmara)
The Turkish automotive hub requires high-strength stainless steel pressings for exhaust system heat shields, deep drawn fuel cell casings, and heavy-vehicle air brake reservoir domes manufactured to strict IATF automotive tolerances.
Strategic Nearshoring Advantages of Sourcing in & Exporter to Turkey
Global supply chain realignments have highlighted the necessity of nearshoring for European and North African B2B buyers. Turkey offers unrivaled supply chain resilience and logistical speed compared to East Asian manufacturing routes:
- EU-Turkey Customs Union Integration: Benefits from the A.TR Movement Certificate, enabling duty-free movement of industrial stainless steel goods across EU member states.
- Rapid Logistics Lead Times: Transit times of just 3 to 7 days by road freight or Ro-Ro shipping lines connecting Turkish ports (Ambarli, Haydarpasa, Alsancak) to major European logistic hubs (Trieste, Rotterdam, Hamburg).
- Decarbonization & EU CBAM Readiness: Modern Turkish manufacturing lines adhere to strict European Green Deal initiatives, utilizing low-carbon scrap steel inputs and energy-efficient hydraulic presses to reduce Carbon Border Adjustment Mechanism (CBAM) liabilities.
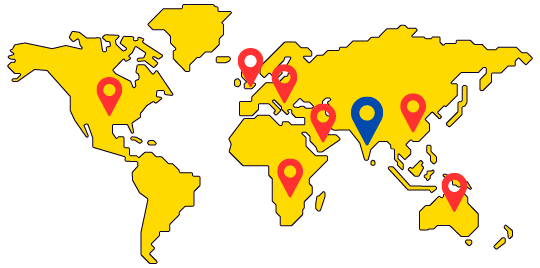
Frequently Asked Questions by B2B Buyers in Turkey & Europe
Clear answers to common questions regarding deep drawing tooling, material certifications, shipping terms, and OEM customization.