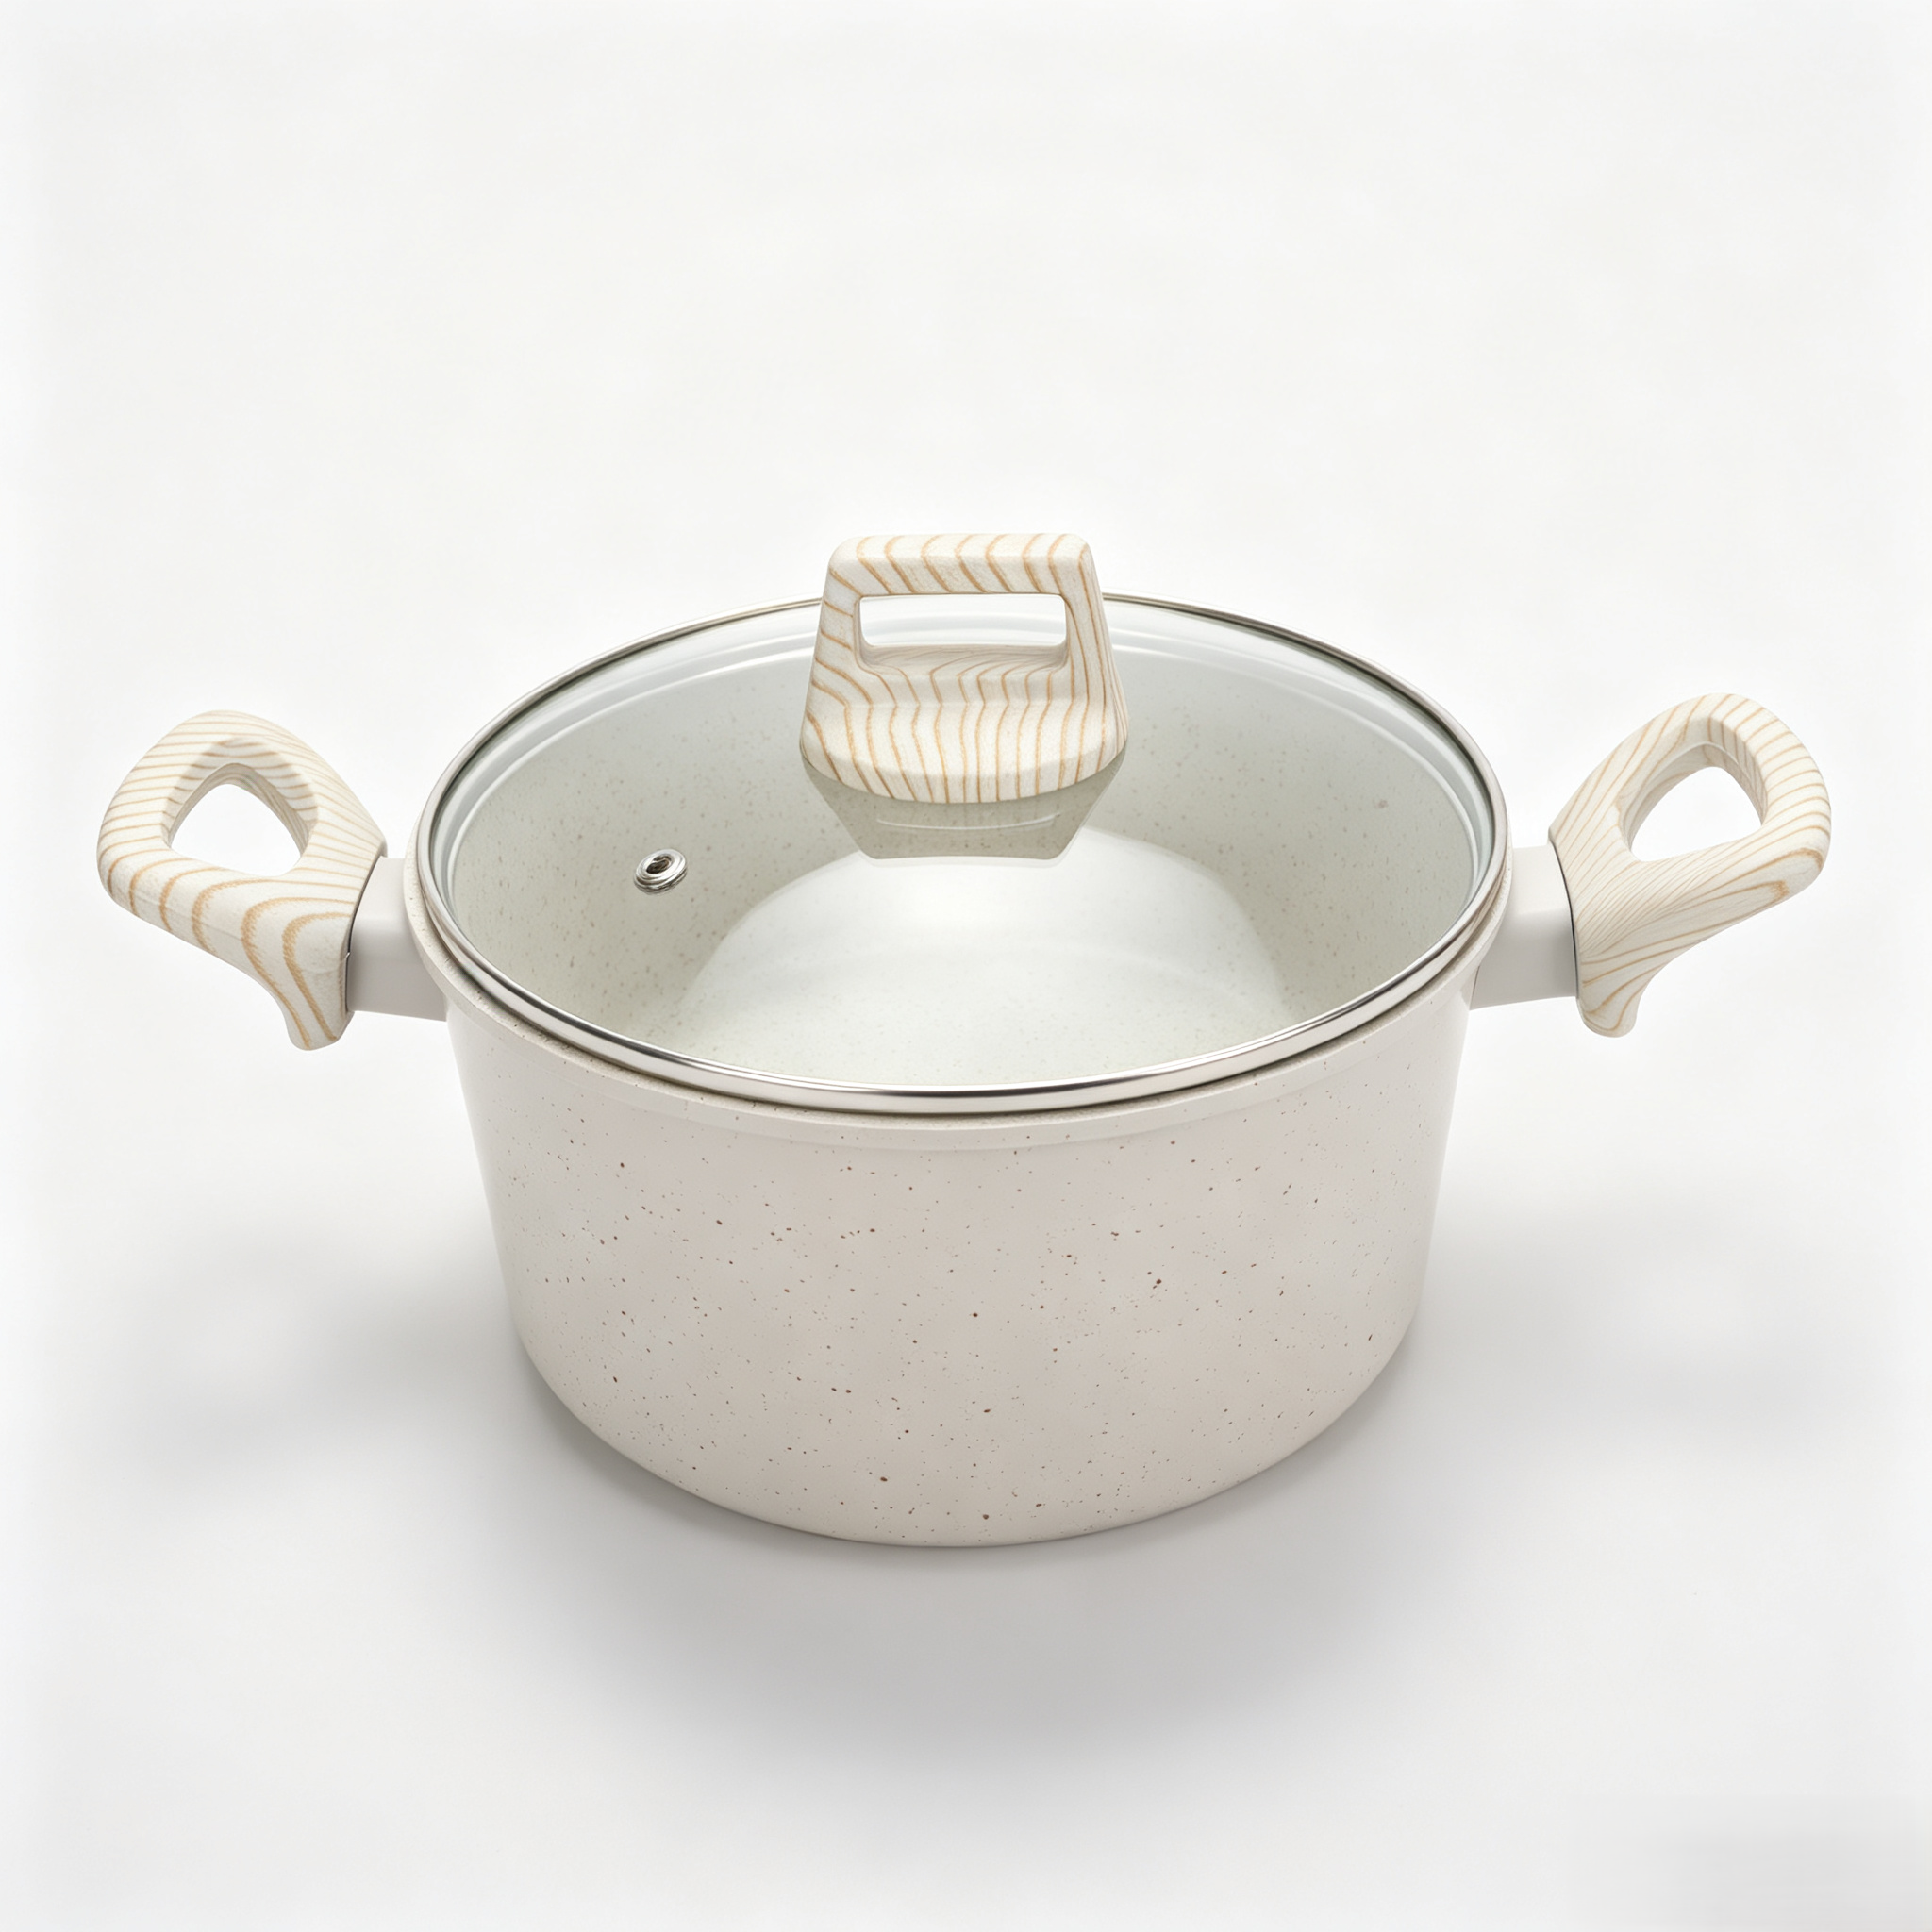
Export Verified Specifications
Industrial-Grade Hard Anodized & Forged Solutions for the UK
Precision tooling, warp-resistant multi-ply substrates, and PTFE/ceramic coating integrity engineered for British induction standards and heavy daily use.
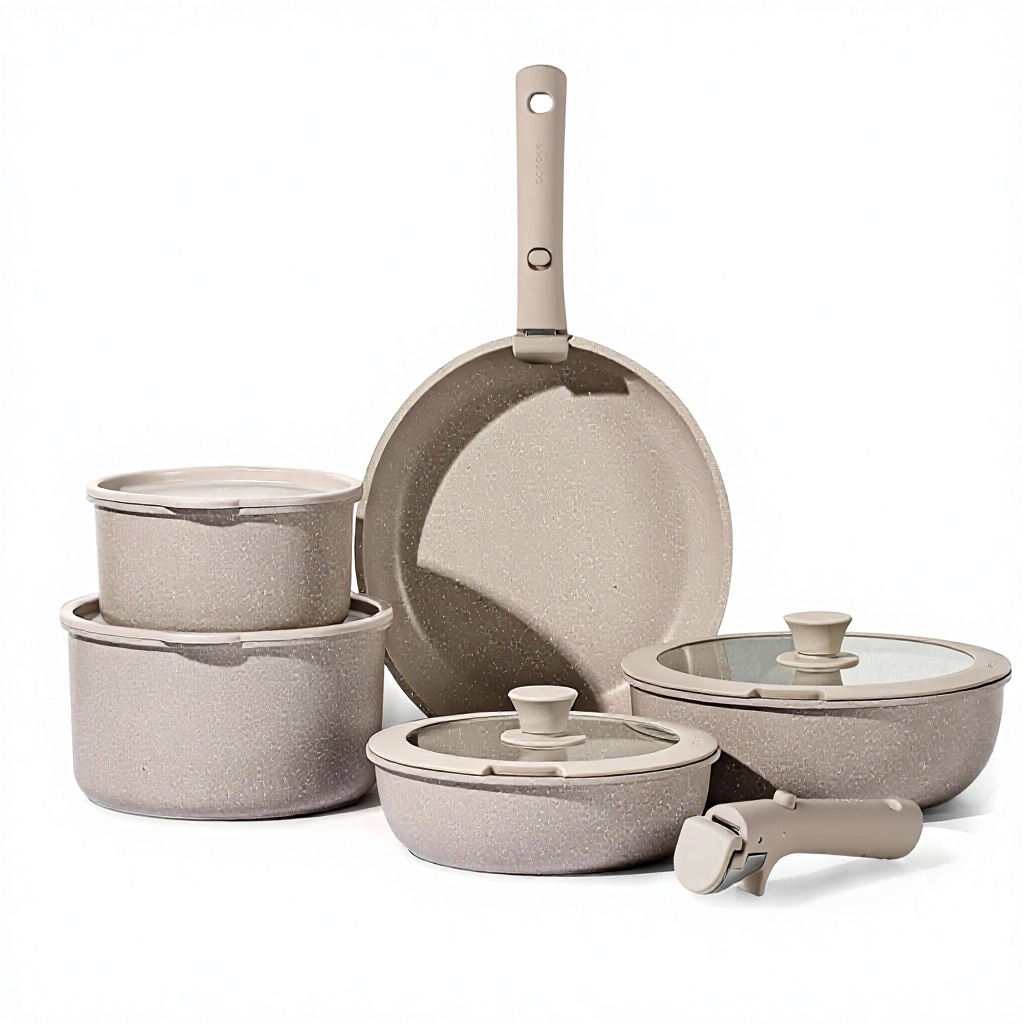
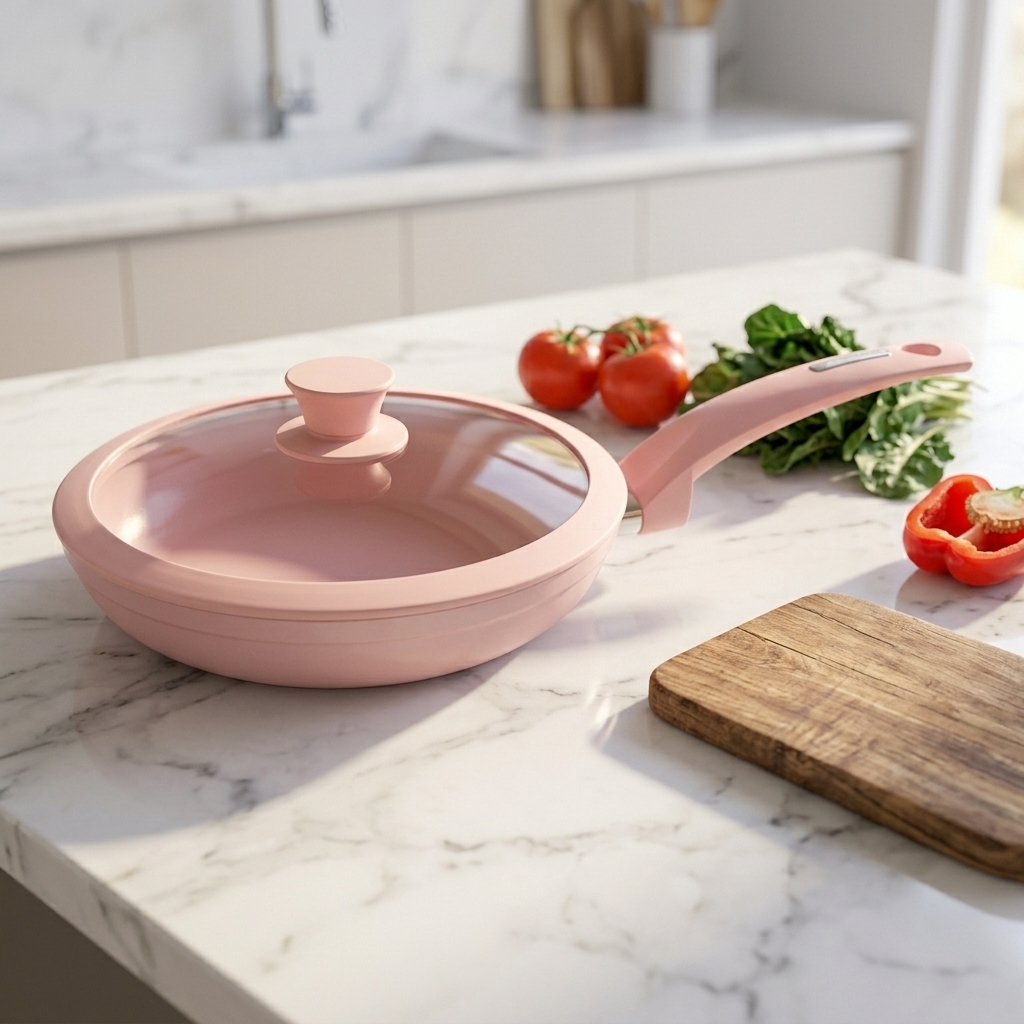
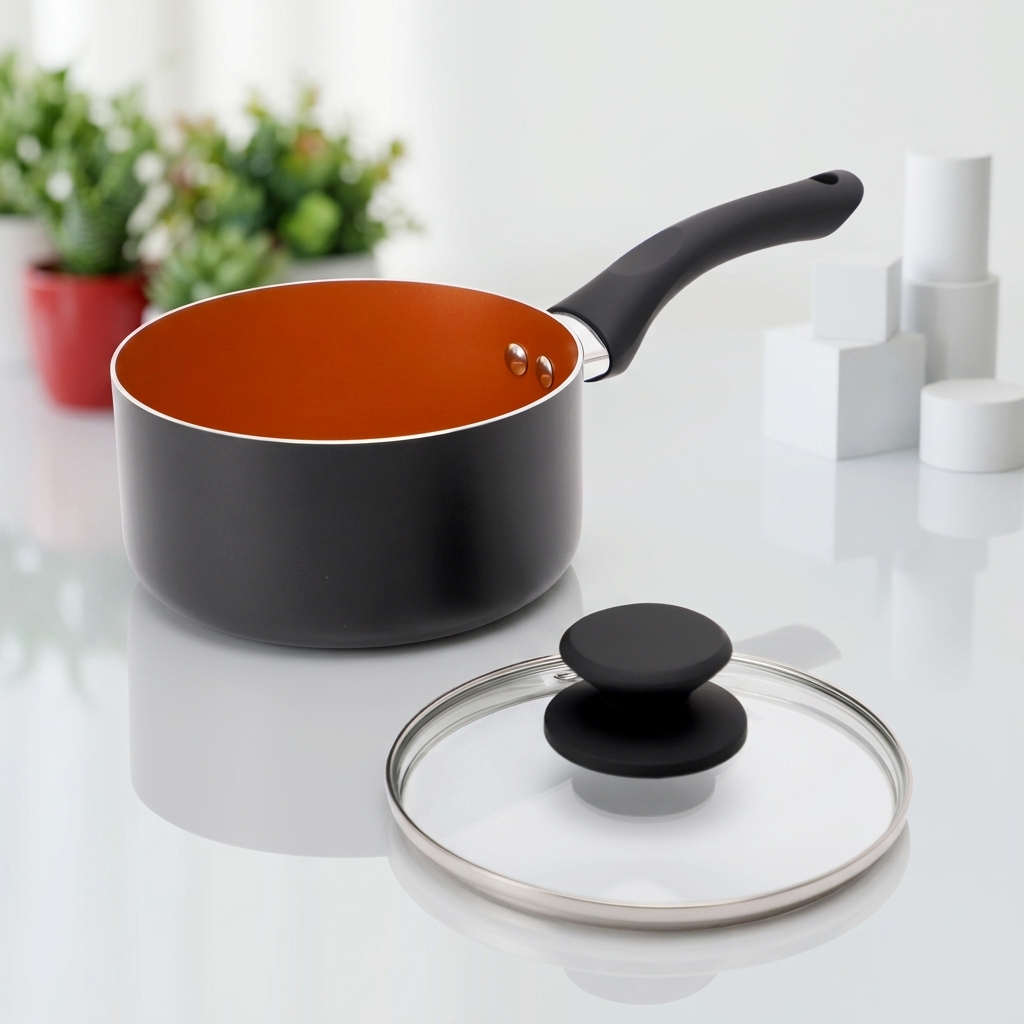
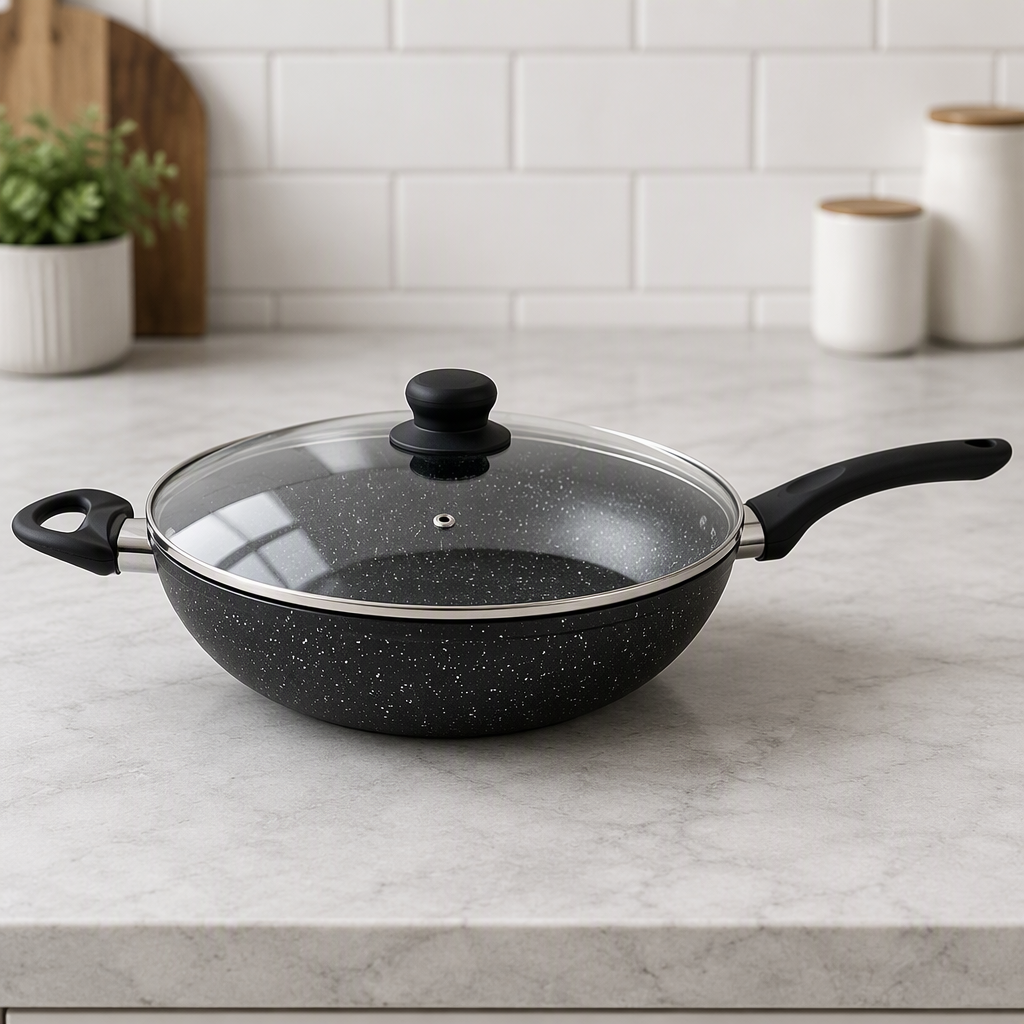
Sheffield’s Metallurgical Heritage Meets Modern Culinary Science: Internationally acclaimed as the historic cradle of British steelmaking and cutlery, Sheffield presents one of the most discerning commercial and consumer houseware markets in the United Kingdom. Retail procurement teams, catering wholesalers across South Yorkshire, and independent boutique brands do not merely purchase cookware; they evaluate metallurgical integrity, molecular grain density, and surface treatment resilience. For modern British culinary workflows—from high-thermal searing to long slow-simmered Yorkshire stews—hard anodized cookware has emerged as the definitive bridge between the extreme thermal responsiveness of raw aluminum and the inert surface hardness of surgical-grade stainless steel.
Regional Market Intelligence
Localization Trends in the Sheffield & South Yorkshire Market
Understanding how energy costs, kitchen space ergonomics, and culinary culture dictate cookware manufacturing specifications in Northern England.
Surging Induction Hob Penetration
Driven by strict UK domestic energy efficiency initiatives and modernized kitchen fittings across Sheffield, over 70% of households are replacing gas with induction. Cookware factories must provide magnetic stainless steel base plates bonded via high-tonnage impact forging to eliminate delamination noise and hot-spot unevenness.
The Demise of "Throwaway" Nonstick
The contemporary British consumer rejects flimsy, stamped 1.8mm pans that warp within months. Buyers across Yorkshire are specifying anodized surface treatments reaching upwards of 40–50 microns, double the hardness of raw steel, ensuring maximum abrasion resistance under standard metal utensil contacts.
Urban Compact Living & Detachable Tooling
With city-center regeneration in Sheffield attracting students, medical professionals, and tech workers to compact apartments, stackable cookware sets featuring quick-release detachable handles (such as CAROTE-style systems) have captured significant retail market share in local department chains.
Technical Benchmarking
Top 10 Hard Anodized Cookware Manufacturing Paradigms
Evaluating primary engineering standards across global OEM/ODM plants serving the UK wholesale ecosystem.
| Evaluation Parameter | Zhejiang MEIS Kitchenware Co., Ltd. | Standard Tier-2 OEM Importer | Conventional Trading Company |
|---|---|---|---|
| Anodizing Process Depth | Electro-chemical Hard Anodized (35–50 µm) controlled in automated tanks | Standard Soft Anodized or Flash Oxidized (<15 µm) | Outsourced third-party coating without depth testing |
| Substrate Architecture | High-density Forged Aluminum (3.5mm–4.5mm rim/base) | Stamped 2.0mm–2.5mm light alloy prone to thermal buckle | Variable, uncalibrated secondary recycled stock |
| Induction Compatibility | Cold-spray / Friction-welded 430 Stainless Disc for 100% flat contact | Punched perforated disc (risk of water entrapment & rust) | Often gas-only unless custom ordered with long lead times |
| Testing Facility & Rigor | In-house TÜV verified labs: Salt Spray, Fatigue, Thrust, Torsion | Visual inspection only; factory certificates rarely verified | Relies entirely on sub-vendor self-declarations |
| Compliance & Chemical Safety | BS EN 12983-1, LFGB, REACH, PFOA-Free Certified | Basic FDA declaration; lacking UK specific audit trails | Inconsistent compliance documentation between batches |
Engineering Excellence: Inside the MEIS Electrochemical Anodization Workshop
Hard anodizing is not simply a decorative coat; it is an electro-chemical transformation that converts surface aluminum into crystalline aluminum oxide (sapphire-grade corundum). At our Jinhua facility, pan bodies undergo sub-zero sulfuric acid baths with carefully monitored current densities. The resulting surface is chemically inert, non-reactive to acidic cooking (such as vinegar reductions or tomato purées favored in classic British gastronomy), and physically fused to the core metal—completely eliminating peeling, blister formation, or delamination under thermal shock.
Vickers Micro-Hardness > 400 HV
Salt Spray Anti-Corrosion > 72 Hours
CNC Laser Planar Base Flattening
Handle Torsion Test Passed @ 150N
Zero Lead, Cadmium & PFAS Leaching
Application Scenarios
Commercial & Domestic Cooking Applications in South Yorkshire
Targeted vessel profiles designed for culinary environments across Sheffield homes, bistros, and institutional catering.
Traditional Sunday Roasting & Braising
From roasting joints of beef to searing mirepoix for rich gravies, our deep anodized casseroles with tempered glass lids provide exceptional moisture retention. The heavy gauge bottom prevents bottom-scorching over long cooking periods on modern low-temperature induction settings.
Gastropub Sear-to-Oven Flexibility
Sheffield’s thriving independent pub and bistro sector requires pans that transition instantly from high-heat stovetop searing to salamander or oven finishing. MEIS cookware engineered with cast stainless steel handles or heat-stabilized Phenolic fixtures withstand oven heats without degrading structural strength.
Direct Manufacturer Advantage
Why Direct Sourcing from Zhejiang MEIS Eliminates Supply Chain Risk
Streamlined manufacturing, full vertical integration, and verifiable operational credentials in Jinhua, Zhejiang.
20-Year Vertical Integration
We are a verified direct manufacturer operating our own heavy hydraulic stamping presses, CNC base processing units, and dust-free automated spray tunnels in Dongnan Industrial Zone. No brokerage markups or opaque third-party sub-contracting.
TÜV Rheinland Audited Facility
Our entire 105-person facility, quality management system, and batch tracking protocols are on-site assessed by TÜV Rheinland. We maintain strict lot traceability from pure A00 aluminum ingots down to final retail carton drop tests.
Agile OEM & ODM Customization
With an in-house tooling, CNC lathe, and mold design workshop, we cut custom profile lead times significantly. Support minor custom runs (logo laser etching, bespoke pantone coatings, retail gift sleeve design) and full mold fabrication for private label lines.
Buyer Knowledge Base
Frequently Asked Questions for Sheffield Sourcing Teams
Practical answers covering compliance, logistics, minimum quantities, and product testing for UK houseware importers.
Does your cookware comply with British Standard BS EN 12983-1 for cookware handles and bodies?
Yes. All MEIS product categories shipped to the UK are engineered in full alignment with BS EN 12983-1 safety requirements. This includes thermal resistance checks for stay-cool bakelite handles, cyclical fatigue loading tests to ensure rivets never loosen during multi-year usage, and static thrust and torsion tests performed on our calibrated on-site lab machinery.
What are your realistic Minimum Order Quantities (MOQs) for UK private-label lines?
For dedicated customized production runs involving custom exterior pantone colors, bespoke packaging, or private-label embossing, our MOQ typically ranges between 1,000 and 2,000 units per size/item. However, for trial market testing or initial SKUs launching on regional eCommerce platforms in the UK, we can accommodate selected models starting from 50 to 500 units utilizing existing in-stock molds.
How does the factory address induction hob efficiency for Northern European markets?
We use specialized 430-grade magnetic stainless steel induction disc plates fused under high tonnage (over 1,200 tons hydraulic impact pressure) directly to the forged aluminum core. This guarantees that our pans do not dome, bow, or buzz when subjected to intense induction hob power spikes, ensuring 100% planar surface contact and rapid energy transfer compliant with UK energy preservation trends.
Are your nonstick coatings 100% PFOA and PFAS compliant with UK REACH regulations?
Absolutely. Every batch of our multi-layer granite, marble speckle, and ceramic nonstick formulations is rigorously tested and certified free of PFOA, lead, cadmium, and hazardous heavy metals. Complete chemical compliance declarations and Migration Test Reports (matching LFGB and UK REACH standards) are supplied directly to your customs and regulatory compliance brokers prior to vessel dispatch.
What is the typical shipping lead time from your Jinhua factory to the Port of Liverpool or Felixstowe?
Our standard production cycle is 35 to 45 days after deposit confirmation and sample approval. Inland transport from our Jinhua plant to Ningbo or Shanghai port takes less than 24 hours. Ocean transit to primary UK ports (Felixstowe, Southampton, or Liverpool) typically averages 28 to 35 days, enabling straightforward quarterly procurement scheduling for Sheffield and Yorkshire distribution centers.
Launch Your Custom Cookware Line with a Verified Manufacturer
Speak directly with our technical engineering desk. Receive complimentary CAD layout reviews, hard-anodized material sample panels, and direct-from-factory FOB quotation sheets within 24 hours.